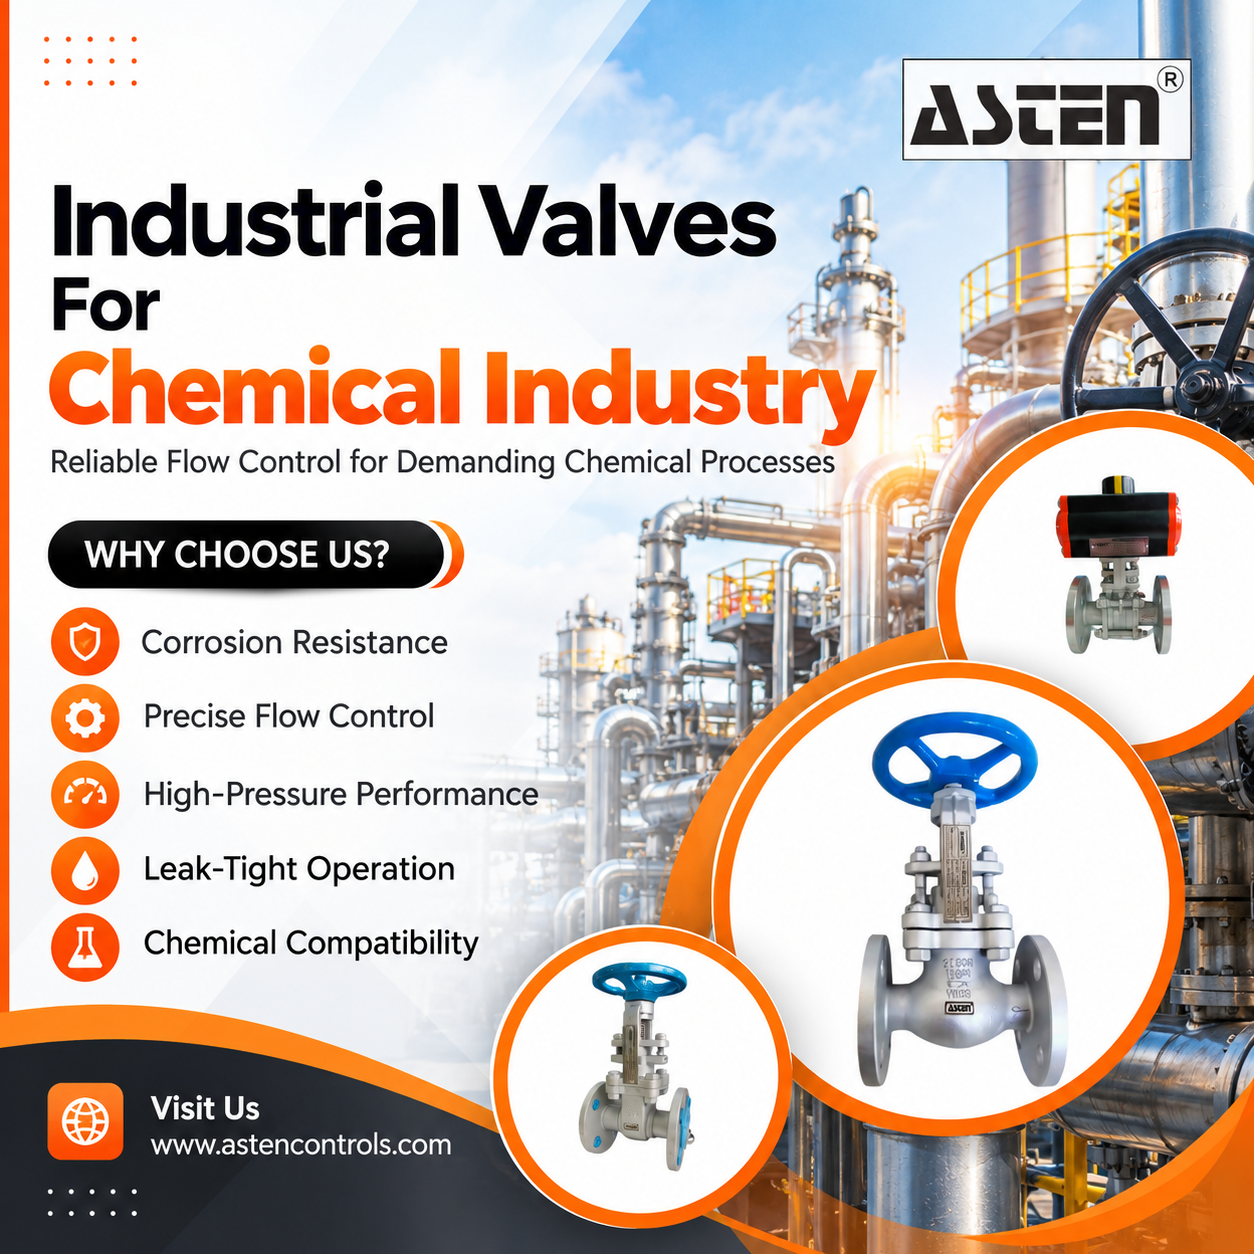
Best Industrial Valve Solutions for Chemical Processing Plants
DescriptionIndustrial Valves for Chemical Industry
Chemical processing plants deal with various liquids, gases, chemicals and process media at different pressures and temperatures. The selection of the appropriate industrial valve is therefore significant in order to control, isolate and direct the flow of process media and ensure effective running of the plant. This is because the right valve should be selected based on the properties of the media, pressure, temperature, flow rate, potential corrosion and the means of operation that are required.
Selection of appropriate industrial valves in chemical processing plants entails considerations of process needs as well as materials of construction. The proper selection of chemical processing industrial valves can help in flow management, equipment protection and isolation of various parts of a chemical processing plant.
Why Are Industrial Valves Important in Chemical Processing Plants?
Valves are very important in any process as they determine the direction and control the flow of process media in pipes and process equipment. Many valves in a chemical plant may serve different purposes.
Flow Regulation
The flow of fluids may need to be controlled at a particular level for some processes. Valves that are used to regulate flows may include control valves.
Flow regulation is very important in some operations such as dosing, chemical reactions, cooling operations, and mixing operations. This will need proper selection of the right valve that can offer the required flow regulation at a certain operating condition.
Process Isolation
It may be necessary to isolate some part of a process during inspection or maintenance. The valves that may be used to isolate some part of the process include gate valves, ball valves, butterfly valves among others depending on the requirement of the pipe and the process.
Process isolation is very important in many chemical plants since various parts of the process may carry corrosive and reactive media.
Pressure Control
Appropriate pressure regulation is critical in many processes involving chemical reactions. Valves can be used in systems which regulate or control process pressures.
This can be done through considering both the normal process pressure, pressure variation and highest expected process pressure.
Protection of Equipment
Using valves for flow regulation and isolation in processes can help protect various equipment from process related damages. For example, check valves can be used to protect equipment against reverse flow.
Careful selection of valves based on process equipment can help avoid flow related operational issues.
Chemical Compatibility
Some of the media in chemical plants may be corrosive, abrasive, toxic or even aggressive in nature. Therefore, chemical processing valves require material selection appropriate for such media.
Material compatibility is a critical factor since exposure to incompatible chemicals can result in corrosion and degradation.
Process Flow Switching
Using valves can allow process flow to be switched to different pipeline, tanks, processing equipment or even process units.
Valve design and type must be chosen based on the flow direction needed and the process conditions.
Automated Process Control
Modern chemical plants are increasingly adopting automated process control systems. Automated process control valves can be used to offer remote operation and control of the flow.
Various types of actuators such as pneumatic, electric among others can be chosen depending on the application.
Key Factors for Selecting Valves for Chemical Processing
Choosing the right industrial valve for a chemical processing plant requires more than selecting a valve based on pipeline size. The process media, pressure, temperature, flow conditions and required valve function should all be considered.
Chemical Compatibility
The valve body, trim, seat, diaphragm, seals and other wetted components should be compatible with the process media. The chemical properties of the fluid should be checked before selecting the valve materials.
Operating Pressure
Check the minimum, normal and maximum operating pressure of the system. The selected valve should be suitable for the expected pressure range to support safe and reliable operation.
Operating Temperature
Temperature can affect valve materials, seals and overall performance. Always consider the minimum and maximum process temperatures when selecting a valve.
Flow Rate and Valve Size
Valve sizing should be based on the required flow rate rather than simply matching the pipeline diameter. Minimum, normal and maximum flow conditions should be considered to achieve suitable flow control.
Corrosion and Material Selection
Corrosive chemicals can affect valve bodies and internal components over time. Material selection should therefore be based on the chemical properties, concentration, temperature and operating conditions of the process media.
Valve Function
The required function helps determine the appropriate valve type. Valves may be selected for:
- Isolation – To stop or allow flow.
- Throttling – To restrict and adjust flow.
- Flow Regulation – To maintain the required flow conditions.
- Pressure Control – To reduce or regulate pressure.
- Backflow Prevention – To prevent reverse flow.
- Automated Control – To operate valves based on process signals or control systems.
Manual or Automated Operation
The choice between manual and automated operation depends on the process requirements, accessibility and frequency of operation. Manual valves may suit simple isolation duties, while automated valves can be useful where remote operation or continuous process control is required.
Best Industrial Valve Solutions for Chemical Processing Plants
Different chemical processes require different valve functions, materials and operating characteristics. Asten Controls offers several industrial valve solutions that can be considered for chemical processing applications, with selection depending on the process media, pressure, temperature, flow and required duty.
Ball Valves for Chemical Processing
Ball valves are commonly used for isolation and quick shut-off in chemical process pipelines. Their suitability depends on selecting body, ball, seat and seal materials that are compatible with the process media and operating conditions.
Butterfly Valves for Chemical Processing
Butterfly valves can be considered for large-diameter pipelines where a compact valve design is preferred. They are commonly used for flow isolation, with material selection based on the chemical, temperature and pressure of the application.
Globe Control Valves for Chemical Process Control
Globe control valves are used where accurate flow regulation is required. They can support pressure and temperature control and are suitable for modulating applications and automated process control systems.
Diaphragm Valves for Chemical Applications
Diaphragm valves can be useful for handling corrosive or chemically aggressive media, depending on material selection. Their design can also help keep the process fluid separated from the operating mechanism, making them suitable for certain chemical and clean-process applications.
Gate Valves for Chemical Processing
Gate valves are generally used for isolation rather than continuous throttling. They can be suitable where the valve is primarily required to provide a full open or full closed flow path in chemical process lines.
Check Valves for Chemical Process Lines
Check valves help prevent reverse flow in chemical process pipelines. They can protect pumps and other process equipment while helping maintain the required direction of fluid flow.
Pressure Reducing Valves for Chemical Processes
Pressure reducing valves are used where the pressure entering a downstream section needs to be reduced and controlled. They can help maintain the required downstream pressure according to the process operating conditions.
Industrial Valve Types for Chemical Processing: Quick Comparison
| Valve Type | Primary Function | Typical Chemical Plant Use |
| Ball Valve | Isolation / On-Off | Process pipelines |
| Butterfly Valve | Isolation / Flow control where suitable | Large-diameter lines |
| Globe Control Valve | Modulating control | Flow, pressure & temperature control |
| Diaphragm Valve | Isolation / regulation depending on design | Chemical and specialised process services |
| Gate Valve | Isolation | Process and utility pipelines |
| Check Valve | Backflow prevention | Pump and process lines |
| Pressure Reducing Valve | Pressure reduction | Pressure-controlled systems |
Where Are Industrial Valves Used in Chemical Plants?
Industrial valves are used all through the chemical plants. Valve type, material and design change depending on the process stage and conditions.
Handling Raw Materials
Raw materials can come in liquid, gaseous form or even other forms and they have to be offloaded into storage tanks or processing equipment. Valves are used for controlling and directing raw materials as they are unloaded and transferred.
The material of the valve should be suitable for the raw material being handled especially if corrosive or reactive.
Chemical Dosing Systems
Chemical dosing is a common process in various chemical and industrial operations. Valves used in chemical dosing systems have to meet the flow control and material handling requirements of the chemical.
For various applications, either precision flow control valves or automatic control valves could be considered.
Reaction and Processing Equipment
Reaction vessels and processing equipment require controlled input and output of process media. Valves are used to control reactants, additives, solvents, gases and other chemicals.
When selecting valves for reaction systems, factors like temperature, pressure, media compatibility and flow control should be considered.
Storage and Transport Systems
Storage tanks and transport pipelines need valves to fill up, empty and isolate the tanks as well as transport products. Chemical plants valves could have different pressure, temperature and media specifications depending on the products stored.
The appropriate valves can help isolate the storage equipment from the rest of the process systems.
Cooling and Heating Systems
Most processes require careful temperature control. Cooling water, cold fluid, thermal fluids and steam may be circulated in the heat exchangers and other pieces of equipment.
Valves will help regulate the media used for heating and cooling as per the temperature required.
Steam and Utility Lines
Chemical plants rely on utilities, including steam, compressed air, cooling water and many others. Valves used in such utility installations include isolation and control valves.
Consideration of pressure, temperature, and properties of utility media should be taken into account when selecting industrial valves.
Wastewater Treatment
Chemical processes may produce wastewater that contains solids, chemicals and other impurities. Valves are used in waste streams and their treatment systems.
Selection of valve materials should be based on the composition and properties of the wastewater.
Chemical Transfer Lines
Transfer lines transport chemicals from tanks, reactors and other vessels in the plant. Transfer lines may require isolation, flow control and routing valves.
In the case of aggressive or corrosive mediums, material selection for valves is especially important.
Material Selection for Chemical Processing Valves
Material selection is one of the main factors that should be considered when selecting chemical processing valves. It includes valve body, trim, seats, seals and other wetted surfaces.
Stainless Steel
Stainless steel is often chosen for chemical processing plants since there are various grades of stainless steel offering good resistance against corrosion and wide operating ranges. The correct grade needs to be chosen based on the type of chemical, concentration, temperature and other operating parameters.
Carbon Steel
Carbon steel could be a good choice for some chemical plants since it offers a sturdy build and is suitable for many industrial purposes. However, the chemical compatibility of the medium needs to be checked before choosing this metal.
Special Alloys When Needed
Some chemical processes require highly corrosive or difficult media for which conventional metals may not be able to offer good service performance. Special alloys or application-specific materials may be required in such situations.
The right material will depend on things like chemical concentration, temperature, pressure, corrosion mechanisms and the expected lifetime.
Seat Materials
Selection of the valve seat is another important consideration. Various seat materials have different characteristics regarding temperature, pressure and corrosion resistance. The correct seat material needs to be chosen depending on the operating medium and conditions.
Valve Seals
The seals of a valve come in contact with the fluid process media, and hence must have proper chemical and temperature resistance properties. An otherwise suitable valve might lead to leaks and deterioration if improper sealing materials are used.
Automated Valve Solutions for Chemical Processing Plants
Valve automation can improve remote operation, process control and repeatability in chemical processing plants. The appropriate automation solution depends on the valve type, process requirements, operating environment and required level of control.
Pneumatic Actuated Valves
Pneumatic actuators use compressed air to operate valves remotely. They are commonly used where fast and repeatable valve operation is required in industrial process systems.
Electric Actuated Valves
Electric actuators use an electric motor to open, close or position a valve. They can be considered where electrical operation, remote control or automated valve positioning is required.
Solenoid Valves
Solenoid valves use an electrically operated coil to control the flow of air or other compatible fluids. They are commonly used as part of automated pneumatic valve control systems.
Valve Positioners and Pneumatic Accessories
Valve positioners help control valve position according to the required process signal, supporting more precise automated regulation. Pneumatic accessories such as air filters, regulators and related control components can support reliable actuator operation.
How to Choose the Right Industrial Valve for a Chemical Plant?
Selecting an industrial valve for a chemical plant requires consideration of the process conditions, valve function and installation requirements. Use the following checklist before finalising a valve:
- Identify the process media: Know the chemical, concentration and physical properties of the fluid.
- Check chemical compatibility: Ensure wetted valve materials are suitable for the process media.
- Determine flow requirements: Consider minimum, normal and maximum flow rates.
- Check operating pressure: Review the minimum, normal and maximum system pressure.
- Check operating temperature: Consider the minimum and maximum process temperature.
- Define the valve function: Determine whether the valve is required for isolation, throttling, regulation or another duty.
- Select suitable materials: Choose body, trim, seat and seal materials based on the application.
- Determine valve size: Size the valve according to actual flow and process requirements rather than pipeline diameter alone.
- Choose manual or automated operation: Consider accessibility, operating frequency and control requirements.
- Review installation and maintenance: Check available space, access and maintenance requirements.
- Consider standards and testing: Verify applicable industry standards, specifications and testing requirements for the application.
Why Choose Asten Controls for Chemical Processing Valve Solutions?
Asten Controls provides industrial valve and flow-control solutions for different process applications, including chemical processing. Its product range and engineering approach allow valve selection to be considered according to the specific operating requirements of each application.
Industrial Valve Manufacturing Experience
Asten Controls has experience in manufacturing and supplying industrial valves and flow-control products for various industrial applications.
ISO 9001:2015 Certification
Asten Controls is an ISO 9001:2015 certified company, reflecting its focus on quality management and consistent manufacturing processes.
Ahmedabad Manufacturing Facility
Asten Controls operates its manufacturing facility in Ahmedabad, Gujarat, providing a local base for manufacturing and supplying industrial valve solutions.
Range of Industrial Valve Solutions
The company offers a range of industrial valves, including ball valves, butterfly valves, control valves, gate valves, check valves and other flow-control solutions.
Control Valve Solutions
Asten Controls provides control valve solutions for applications where accurate flow, pressure or process regulation is required.
Automation and Pneumatic Accessories
Its valve solutions can also include automated operation and pneumatic accessories for applications requiring remote or controlled valve operation.
Application-Based Valve Selection
Valve selection can be based on factors such as process media, pressure, temperature, flow requirements and the required valve function.
Engineering Support
Asten Controls provides engineering support to help identify suitable valve solutions according to the operating and application requirements of the process system.
Frequently Asked Questions about Valves for Chemical Processing
What types of valves are used in chemical processing plants?
Butterfly valves, ball valves, gate valves, globe valves, check valves, diaphragm valves, control valves are some commonly used types of valves in such plants.
How do I select a valve for my corrosive chemical application?
Take into consideration the chemical nature and strength of the fluid, the temperatures and pressures that will prevail, what valve function is needed, and the body material, trim materials, seat material and seals. Special materials may be needed for highly corrosive applications.
What is the right valve for chemical process flow control?
Selection of an adequate valve depends on the flow range, the pressure drop, the process medium, and the degree of regulation needed. Generally, control valves are used for continuous automatic regulation. Other regulating valves can serve for certain applications.
What considerations apply to the selection of chemical process valves?
These include the process medium, flow rate, pressure, temperature, corrosion, valve size, connections, material compatibility, flow characteristics, operating frequency, actuators, and installation.
Are automated valves suitable for chemical processing plants?
Yes, automated valves can be suitable where remote operation, frequent cycling or automated process control is required. The actuator and valve should be selected according to the process conditions and application.
Why is valve material important in chemical processing?
Valve materials must be compatible with the process media to reduce the risk of corrosion, degradation and premature component failure. Material selection should consider the chemical, concentration, temperature and operating conditions.
What is the difference between isolation and control valves?
Isolation valves are primarily used to start or stop flow, while control valves are designed to regulate flow, pressure or other process conditions. The choice depends on the required function of the system.
Need Industrial Valve Solutions for Your Chemical Processing Plant?
Choosing the proper valve for a chemical process application involves many aspects such as media, pressure, temperature, flow needs, and material compatibility. Each particular location in the plant will need its own valves.
Let us know what your application demands in order to recommend an appropriate valve for your process. As an industrial valve manufacturer in India, we can assist you in determining the kind of valve that will suit your process application.


